Water is the largest contaminant a compressed air system has to deal with, and Singapore hands every plant a generous supply of it. Air drawn into a compressor here is warm and close to saturation for much of the year, and every cubic metre of it carries moisture that has to go somewhere once the air is compressed and cooled.
Where that water ends up decides whether the system runs quietly in the background or produces a steady trickle of rusted fittings, sticking valves, spoiled coatings and rejected product. Dryer selection is the control point, and it deserves more attention than a line item at the end of a compressor quotation.
Why Tropical Air Loads the System
Compression concentrates moisture. Air at ambient conditions holds a certain mass of water vapour, and squeezing it into a fraction of its original volume raises the vapour concentration well past saturation once the aftercooler brings the temperature back down. The excess leaves as liquid water, and the volumes involved surprise people who have not measured them.
Ambient conditions here make the effect more pronounced than in temperate climates. High year-round humidity means the intake air is close to its dew point before compression even begins, so an air compressor generates more condensate per unit of delivered air than the same machine would in a cooler, drier location.
The aftercooler and receiver remove a large share of that water, but not all of it. Air leaving a receiver is still saturated at whatever temperature it has reached, so any further cooling downstream, in a long run of pipework across a factory roof at night, for instance, produces more liquid at exactly the point where equipment is connected.
Pressure Dew Point, Not Relative Humidity
The number that governs air dryness is pressure dew point, the temperature at which water begins to condense out of the air at system pressure. As long as the air in the pipework never falls below that temperature, it stays dry.
Relative humidity is unhelpful here, because the same air expressed as a percentage means different things at different pressures and temperatures. Specifying a pressure dew point at the working pressure removes the ambiguity, and it is the figure every dryer datasheet is built around.
How the Purity Classes Are Written
Air quality is described by ISO 8573-1:2010, which sets out purity classes for particulate, water and oil content in that order. The humidity classes are defined by pressure dew point: Class 1 below minus 70 degrees Celsius, Class 2 below minus 40, Class 3 below minus 20, Class 4 below plus 3, Class 5 below plus 7 and Class 6 below plus 10. A requirement quoted as Class 1 for particulate, Class 4 for water and Class 1 for oil is written as a set of three numbers, which makes tender comparison far simpler once everyone uses the same notation.
Refrigerated Dryers and Where They Stop
A refrigerated dryer chills the air stream to condense out water, separates the liquid and reheats the air slightly to prevent sweating on the outside of the pipework. The achievable dew point is limited by the need to avoid freezing the condensate on the heat exchanger surface, which places these units in Class 4 territory for typical selections.
For general workshop air, pneumatic tools, clamping, blowing and most production duties, that is entirely adequate and it is the most economical way to get there. Cycling designs reduce energy consumption at part load by storing cooling capacity in a thermal mass, which suits plants whose air demand varies through the shift.
Desiccant Drying for Lower Dew Points
Applications that cannot tolerate any liquid water, or that run pipework through spaces cold enough to reach freezing, need adsorption drying. A desiccant dryer passes air over a bed of hygroscopic material while a second bed regenerates, alternating between them, and reaches dew points well below anything a refrigerated unit can offer.
Instrument air, outdoor pneumatic controls, pharmaceutical and electronics processes, powder handling and paint finishing all commonly specify Class 2 or better. The trade-off is energy and air consumption during regeneration, since heatless designs use a portion of the dried air to strip moisture from the offline bed, and that purge flow has to be added to the compressor sizing rather than discovered later.
Heated and blower purge variants reduce the purge penalty at the cost of additional equipment and controls. Choosing between them is a straightforward comparison once the required dew point, the flow and the duty cycle are known, and it should be made before the compressor is sized.
Sizing for Real Site Conditions
Dryer ratings are published at reference conditions, and a plant room in a Singapore industrial estate on a September afternoon is not the reference condition. Capacity falls as inlet air temperature, ambient temperature or operating pressure move away from the rated values, so the selection has to be checked against site data using the manufacturer’s correction factors.
Gather the following before asking for a selection:
- Actual air demand in free air delivered, including any regeneration purge
- Minimum operating pressure at the dryer inlet
- Compressed air temperature entering the dryer after the aftercooler
- Plant room ambient temperature at its warmest, not its average
- The pressure dew point the most demanding application on site requires
Filtration, Drains and Condensate
Filtration order is not arbitrary. Coalescing filters upstream protect the dryer from oil aerosols and bulk liquid, particulate filters downstream catch desiccant dust, and drains at every low point remove what has separated. Timer drains discharge air along with water, while zero-loss designs open only when liquid is present, which is a small saving repeated thousands of times a day. Teams that already handle condensate in their air compressor systematically will find the same instincts apply to drying, since both come down to removing water at the right place and disposing of it properly. Condensate carrying oil is subject to PUB’s trade effluent requirements before it reaches a sewer, which makes an oil and water separator part of the system, not an accessory.
Judging the Energy Cost of Drying
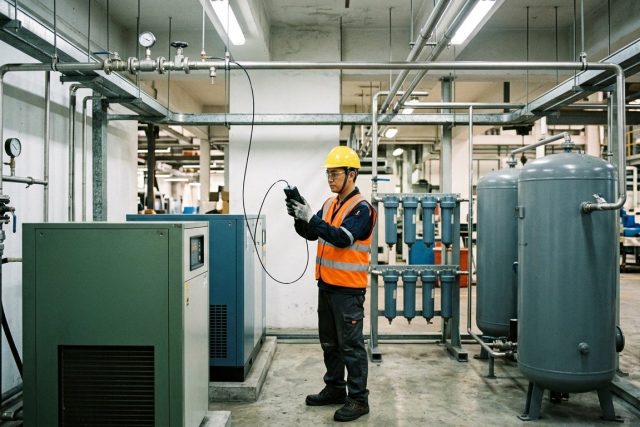
Every element in the treatment train costs pressure, and pressure costs power. A blocked filter, an undersized dryer or a poorly routed header quietly raises the discharge pressure the compressor has to hold, and the effect on the electricity bill is continuous. Measuring differential pressure across the treatment train, and acting on it, is among the simplest energy improvements available in a plant room.
An air compressor audit puts numbers to that, logging demand, pressure and specific power over a representative period so decisions rest on measurement instead of assumption.
Getting the Air Quality You Actually Need
Specifying air quality is a question of matching the dew point to the most demanding application, then sizing for the conditions the plant room really sees. Over-specify and the plant pays for dryness nobody uses; under-specify and the cost arrives later as corrosion and downtime.
Our WE Supply team can help you work through the numbers, and WE Service supports treatment equipment once it is installed.
If you are planning a new compressed air installation or reviewing one that is not holding the quality it should, get in touch with Winston Engineering and we will help you size the treatment to the duty.
Author Bio
Team Winston Engineering

Team Winston Engineering is made up of pump specialists, engineers, and industry experts with over 40 years of hands-on experience in fluid management solutions. Founded in Singapore in 1977, Winston Engineering has grown into Southeast Asia's leading pump specialist, serving industries ranging from oil and gas to water treatment, HVAC, and power generation. With regional offices across Singapore, Malaysia, Indonesia, and China, the team brings deep technical expertise and a customer-first approach to every project, backed by the region's only state-of-the-art pump test bay.
See all posts by Team Winston Engineering »